If you’ve ever picked up a cereal box, a medicine bottle sleeve, or a gourmet coffee pack that folds flat for shipping, you’ve held a folding carton—one of the most ubiquitous, hardworking, and often underappreciated packaging materials on the market. As a folding carton supplier of 12 years, I’ve walked shop floors, troubleshooted runs, and talked through design tweaks with every type of brand, from small-batch craft chocolate makers to national pharmaceutical chains. It’s easy to take these lightweight, functional packages for granted, but their journey from a roll of paperboard to your hands is a tightly calibrated mix of engineering, craftsmanship, and quality control. Let me walk you through exactly how a folding carton is made, straight from the people who build them every day. Folding Carton
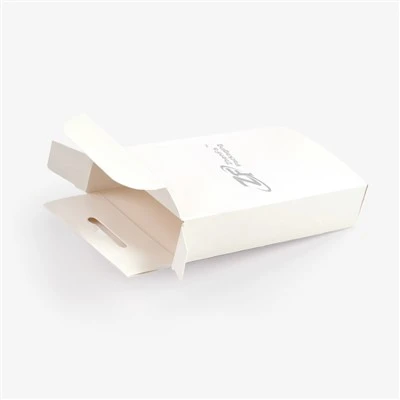
It all starts before any ink hits paper, though. The first step in our process is often forgotten, but it’s the foundation of every carton: material selection. Folding cartons aren’t just “cardboard”—that common term refers to corrugated material, which is far too thick and rigid for most retail packaging. We rely on paperboard, a thick, dense fiber product with a basis weight typically between 12 and 40 points (a measurement of thickness where 1 point equals 0.001 inch). The right grade depends entirely on what the carton needs to do. If you’re building a box for a 100mg prescription pill, you need a solid bleached sulfate (SBS) board—bright white, smooth, and resistant to moisture and light, which protects light-sensitive drugs. For a craft beer six-pack sleeve, we might use a coated unbleached kraft board for a rustic, earthy finish that’s durable enough to handle shelf handling without tearing. For frozen food, we choose a grease-resistant coated board that stands up to condensation. We source our board from mills with strict chain-of-custody certifications, too, because brands big and small care about ethical and sustainable materials these days. No matter the grade, we always pull sample rolls to test for bending stiffness, surface smoothness, and ink adhesion before a single production run starts—one bad roll can waste hundreds of hours and thousands of dollars.
Once the material is approved, we move to the first of our in-house manufacturing steps: die cutting, also called blanking. The paperboard is fed into a large rotary die cutter or a flatbed die cutter, depending on the order size. Rotary cutters are used for high-volume runs (think 100,000 cereal boxes), where the board is fed in a continuous roll, and a sharp, cylinder-mounted die cuts the flat, unassembled carton “blanks” to their exact shape. Each blank has pre-scored lines, too—tiny, shallow cuts that don’t go all the way through the board, which let the carton fold cleanly later on. Flatbed die cutters, used for smaller custom runs (like 5,000 luxury candle cartons), use a custom steel rule die pressed against the board, creating more intricate shapes, custom windows, and unique fold patterns that rotary dies can’t pull off. If a brand wants a window to show off their product (think a chocolate bar carton with a clear plastic window), we add that step here too: a machine cuts the window opening in the blank, then we heat and adhere a thin film of biaxially oriented polypropylene (BOPP) plastic over the opening. It’s a precise job—too little adhesive and the film will fall off during shipping, too much and it wrinkles.
Next up: printing and coating, the step that turns a plain brown or white blank into the branded package you recognize. Folding carton printing is almost always done with flexographic presses, though some high-end custom jobs use offset lithography for ultra-smooth, vibrant finishes. Flexo uses flexible rubber plates that wrap around cylinders, transfer ink to an anilox roller, and then apply it to the paperboard—fast, cost-effective, and perfect for large runs. For our team, color accuracy is non-negotiable. We use a Pantone color matching system, so a brand can specify exactly the shade of blue for their logo, and we test the press’s output against a physical color swatch before we run the full order. No one wants a batch of cartons where the cereal mascot’s face is off by three shades.
After printing, we add coatings to protect the design and the carton itself. If a carton is going through a commercial dishwasher (think a frozen meal pack), we apply a water-based barrier coating to prevent grease and moisture from seeping through. For luxury cartons that need a premium, shiny finish, we add a gloss or matte aqueous coating, which dries quickly and adds a sleek feel without the harsh chemicals of old varnishes. Some brands also ask for a UV coating, which adds extra durability for products that will be stored outdoors, or a soft-touch coating for cosmetics packaging that feels nice to hold. Every coating is tested for adhesion too—we rub the carton with a tape and make sure the ink and coating don’t peel off, a common complaint from brands that cut corners on coating quality.
Once the ink and coating are dry, we move to the final manufacturing step before shipping: blank preparation and finishing. Wait—isn’t assembling the carton part of it? Yes, but the actual folding and gluing happens in a machine called a folder-gluer, which is the heart of our shop floor. When the blanks come out of the printing and coating area, they’re stacked and fed into the folder-gluer in a continuous stream. The machine first folds the scored lines automatically, then applies hot melt adhesive to the tabs that hold the carton together (usually the side seams, or the bottom flaps that will hold the product inside). It’s a fast process—some folder-gluers can produce over 500 cartons per minute, which means a small run of 10,000 cartons is done in less than 20 minutes. For specialty cartons, like those with interlocking closures or child-resistant flaps (a must for pharmaceutical and household cleaning products), the folder-gluer is programmed to create those custom features without extra steps. We have operators who monitor every run here, because a misaligned fold or a missed glue spot can ruin an entire batch. If a carton folds wrong, it can jam the machine, damage the blanks, or end up as a defective package that won’t hold its product.
Once the cartons are folded and glued, they’re stacked, strapped, and palletized, ready for shipping. Wait, but what about the “flat” packaging you see? Folding cartons are designed to collapse flat for storage and shipping, which is one of their biggest advantages over rigid boxes. They take up 75% less space in warehouses and trucks, cutting down on shipping costs and environmental waste compared to pre-assembled boxes. That’s why you never see a full cereal carton sitting on a store shelf folded flat—they’re pre-assembled at the supplier, then sent to the retailer ready to hold product.
Of course, this process doesn’t happen without a lot of behind-the-scenes quality control, which is what makes a good folding carton supplier different from a mediocre one. Every batch goes through three inspection points: first, a visual check for print defects (smudges, faded colors, misaligned graphics), second, a structural test where a worker pulls a carton open, fills it with a standard weight, and drops it from 3 feet to make sure it doesn’t split, and third, a random sample test where we keep a carton for six months to check for ink fading or coating durability, especially for outdoor products. We also keep records of every run—what board was used, what colors, what machine it ran on—so if a brand notices an issue six months down the line, we can trace it back immediately.
Over the years, I’ve seen folding cartons evolve a lot, too. Ten years ago, most cartons were made with standard SBS board and basic print. Now, brands are asking for more sustainable options: recycled paperboard (we use post-consumer recycled content for 60% of our standard runs), water-based inks instead of solvent-based ones, and cartons that are 100% recyclable or compostable. We’ve invested in new machinery that can handle thin, lightweight board that cuts down on material use by 15% without sacrificing strength. Even small brands, like artisanal jam makers or local pet treat companies, are asking for custom window cuts, embossed logos, and hand-finished details that used to be only for big national brands. That’s the great thing about folding cartons—they’re versatile enough for every budget, every product, and every brand’s identity.
If you’re a brand owner, a retail buyer, or someone who’s spent years working with packaging, this process might sound familiar, but I hope I’ve given you a better sense of the precision and care that goes into every carton. It’s not just paper and glue—it’s the end of a long chain of decisions: picking the right board to protect your product, getting the colors right to match your brand, making sure the carton holds up to being shipped, stored, and opened by your customers. At the end of the day, a folding carton is a silent workhorse—it doesn’t call attention to itself, but it’s the first thing your customer touches, and it’s the last thing that protects your product from the shelf to their kitchen counter.
If you’re looking for a reliable folding carton supplier, whether you need a small custom run for a new product or a large bulk order for a national launch, reach out to our team to discuss your needs. We can walk you through material options, design tweaks, and cost-saving solutions that fit your timeline and budget.
Folding Carton References
- Soroka, W. (2008). Fundamentals of Packaging Technology. Institute of Packaging Professionals.
- Tuck, G. (2016). Folding Carton Manufacturing: A Guide to Materials and Processes. Packaging Technology and Science.
- Sustainable Packaging Coalition. (2022). Folding Carton Sustainability Report.
Wenzhou Zhenfa Packaging Co., Ltd.
As one of the most professional folding carton manufacturers and suppliers in China, we have world-leading production equipment and strong manufacturing capabilities. Please feel free to wholesale bulk advanced folding carton in stock here from our factory. Also, quotation is available.
Address: Room 105, Building 10, Century Science and Technology Entrepreneurship Park, Longgang City, Wenzhou City, Zhejiang Province
E-mail: ZhenfaPackaging@outlook.com
WebSite: https://www.cnzhenfa.com/
